Mechanical disturbance
Conveyor contact, flexible hoses, nearby machinery, operator touch and unstable pallets can all appear as changing weight.
A net-weight filling machine places the container on a weighing system, records or applies the tare, then stops product flow when the target net mass is reached. It is especially useful when weight is the controlling quantity, container tare varies, or a larger pack needs direct weighing during filling.
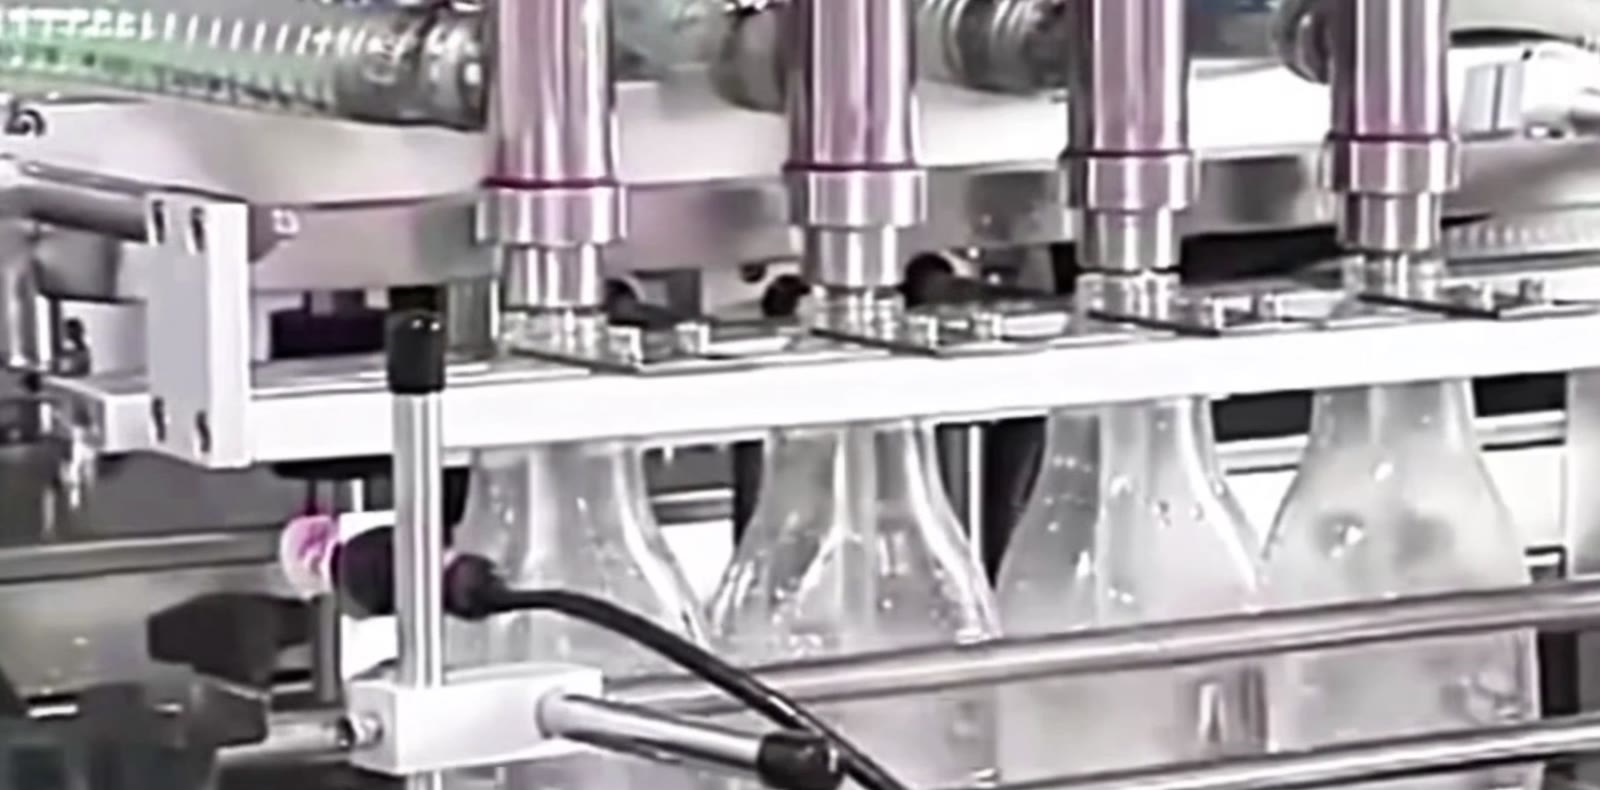
Net-weight filling uses a load cell or weighing platform to control the mass of product added after accounting for the empty container. The method can reduce sensitivity to container internal volume and product density, but it requires stable tare handling, controlled product cut-off and protection from vibration.
The filler does not remove the packer’s responsibility for quantity control. Machine settings, independent checks, records and the applicable legal system still need to be defined by the business.
The pack, pallet or platform must settle without conveyor impact or operator contact disturbing the signal.
The system records the empty-container weight or applies a verified tare method before adding product.
A bulk stage delivers most of the product while controlling splash, foam and container stability.
A slower stage reduces overshoot caused by valve response, liquid in flight and product remaining in the nozzle.
The accepted process defines whether every pack is measured, whether samples are checked and which records are retained.
| Application | Potential advantage | Important boundary |
|---|---|---|
| Oils and lubricants | Weight control can remain useful where density or temperature varies and larger packs are involved. | Nozzle residue, viscosity and safe pack movement still affect the cycle. |
| Pails and drums | The container can remain on a weighing platform during filling. | Pallet, operator and hose forces must not disturb the scale. |
| High-value liquids | Direct measurement can support tighter giveaway control when the product and checking system justify it. | The full process capability must be demonstrated; a quoted scale resolution is not a package guarantee. |
| Variable-tare containers | Individual tare can reduce the effect of empty-pack weight variation. | Tare capture adds time and must be protected from unstable containers or debris. |
Conveyor contact, flexible hoses, nearby machinery, operator touch and unstable pallets can all appear as changing weight.
Liquid continues moving between the shut-off point and container. Fast/slow control and valve position must account for that material.
Container, lid, pallet and label components must be included or excluded consistently according to the quantity definition.
Product added after the accepted weight can create overfill, dirty packs or a mismatch between machine and downstream checks.
Great Britain packaged-goods rules place responsibility on the packer or importer to use suitable equipment, control quantity and keep required records. The relevant route may be the minimum system, the average system or another application-specific control. Consult competent metrology or Trading Standards advice where the duty is unclear.
Useful official references include GOV.UK packaged-goods guidance and equipment and records guidance.
A net-weight filling machine supports the container on a load cell or weighing platform, establishes the empty-container tare and adds product until the required net mass is reached. The controller normally uses a faster bulk stage followed by a slower final stage so the product path can close without excessive overshoot.
Net weight is the product mass without the container, while gross weight includes the container and product together. A net-weight system must account for tare variation before or during the cycle. A gross target can be used only where the container tare and quantity-control method make it appropriate.
Weight filling may be preferable where the sale or process is controlled by mass, density changes make volume less convenient, container tare varies, or large containers are already handled on a scale. Volumetric filling may be faster or simpler for stable liquids and smaller packs. The correct comparison uses the real product, pack and checking method.
A weighing system measures force, so conveyor impact, flexible hoses, pumps, operator contact and nearby machinery can disturb the signal. The container support, isolation, fill hose and line sequence must allow the weight to settle sufficiently for the agreed control and verification method.
Net-weight filling is often considered for pails, drums and IBCs because the container can be supported on a platform while product is added. The project still needs safe nozzle access, tare handling, fast and slow flow stages, overfill protection, pallet or conveyor movement and a defined method for checking the result.
No. The machine is one part of the packer’s quantity-control system. The business remains responsible for choosing suitable equipment, checking packages, keeping required records and meeting the applicable minimum or average system. The final compliance route should be agreed with competent metrology or Trading Standards advice where needed.
Lancing can compare practical machine routes, identify what can be quoted from the available information and define where samples or a representative trial are needed.
Send the product, pack and output details that matter. We’ll compare the most practical dosing and line options for you.